“EPC contractors standardise India’s thermal ecosystem,” Agarwal
Salasar Techno Engineering outlines how integrated heavy structural steel manufacturing supports India’s thermal power expansion.
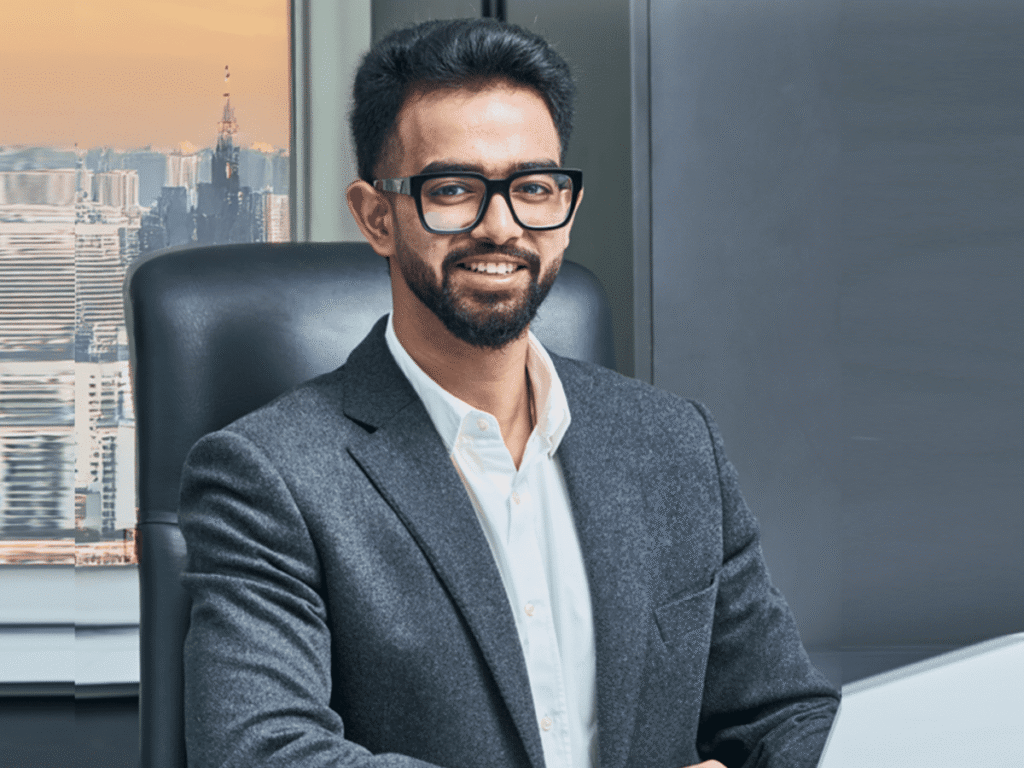
Bharat Agarwal, President Heavy Structures Division, Salasar Techno Engineering
India’s infrastructure and energy landscape is undergoing a major transformation, driven by rising power demand, industrial expansion, and the transition towards a more resilient energy ecosystem. As the country scales up thermal capacity alongside renewable growth, the demand for advanced engineering, manufacturing capabilities, and reliable structural solutions is becoming increasingly critical.
Heavy structural steel plays a vital role in supporting large-scale power projects, from boiler structures and turbine halls to associated plant infrastructure. Companies with integrated design, fabrication, and execution capabilities are positioned to address the evolving needs of the sector while adapting to higher efficiency standards and changing project requirements. In this interview, Bharat Agarwal, President of the Heavy Structures Division, Salasar Techno Engineering, shares insights into the company’s manufacturing capabilities, industry trends, and the future of heavy structural solutions in India’s evolving energy landscape.
How has Salasar positioned its manufacturing capabilities to meet the demand for boiler support structures amid India’s 97 GW thermal capacity target by 2034–35?
The 97 GW thermal capacity addition target is one of the most consequential infrastructure mandates India has set in recent memory.
Our decision to commission a dedicated heavy structural steel manufacturing facility at Hapur, Uttar Pradesh, alongside the phased expansion of our Bhilai operations, adding 1,000 MT capacity by the end of Q2 and a further 1,000 MT by Q4 was precisely calibrated to serve this demand, covering boiler support structures, turbine hall frames, coal handling plant steel, and associated thermal plant infrastructure.
The plant is equipped with one of Asia’s widest galvanising facilities, powered by a 13m long bath for peak-throughput operations. What distinguishes us is the integrated model – engineering, detailing, fabrication, and dispatch all under one roof – which eliminates interface delays. At the scale of new 660 MW and 800 MW supercritical units, a boiler structure can weigh upward of 2,000 – 3,000 MT; co-located engineering and manufacturing capability is not a luxury; it is a competitive necessity
What design changes in modern thermal plants, such as higher-efficiency supercritical units, influence your fabrication processes and material specifications?
Supercritical and ultra-supercritical units operate at efficiencies of 38-45 per cent depending on design – and the structural envelope of these plants is considerably more demanding than subcritical predecessors. A 660 MW or 800 MW USC boiler can exceed 100 metres in height, requiring structures engineered for simultaneous static loads, dynamic thermal expansion, seismic forces, and wind loading. Welding of high-temperature alloy steels including P91 and P92 grades represents a specific challenge in the supercritical fabrication space. While our scope is primarily the structural envelope, our detailing and weld procedures must account for thermal movement of pressure parts without imposing constraint loads on the structure. We have updated our design software suite – Tekla and STAAD. Pro and ETAB – and our welding protocols accordingly.
Can you detail engineering challenges in delivering structures for Adani and L&T projects, particularly tolerances for heavy lifts and seismic compliance?
Our scope on these projects is manufacturing and supply; we fabricate to client-issued engineering drawings, which means accountability for dimensional accuracy and quality rests entirely with us at the production stage. There is no downstream correction opportunity; misalignment during heavy lifts of 200–300 MT becomes a site problem that is disproportionately expensive to resolve compared to catching it at the fabrication stage.
To further ensure on-site erectability, we carry out shop assembly of critical structural elements, such as columns, before dispatch. This pre-assembly step validates fit-up and alignment under controlled conditions so that what reaches the site goes up without surprises.
On seismic compliance, we adhere to IS 7215 for fabrication tolerances, and our manufacturing processes are fully aligned with the load combination requirements of IS 1893 for Zone III and Zone IV sites. Connection geometry, gusset configurations, and weld quality are all produced and inspected with that loading environment in mind. All critical welds undergo non-destructive testing as standard.
How do lead times and supply chain bottlenecks for high-tensile steel impact delivery schedules for projects under construction?
Across India’s power infrastructure sector, component availability is lagging demand, creating mounting stress across supply chains – and structural steel sourcing is no exception. High-tensile steel grades standard for boiler support structures are not universally available off the shelf, and when multiple large thermal projects run simultaneously, mill queues lengthen significantly. Geopolitical disruptions have further tightened supply, pushing up costs and delivery uncertainty for iron ore and scrap imports.
Our mitigation is twofold: we place steel orders at engineering completion – design intent is sufficient to lock in tonnage and grade – and we maintain long-term supply relationships with primary producers, keeping us out of spot allocation queues. A working stock buffer of commonly used sections provides an additional 4–6 week cushion during tight markets.
What investments in plant automation or welding technology support scaling production for the 38 GW pipeline?
Our Hapur facility is equipped with CNC-controlled beam processing lines – drilling, milling, and marking – which reduce setup time and improve dimensional accuracy significantly. The centrepiece is our Coreimpex beam welding machine, which delivers high-precision, high-throughput performance on heavy structural members with consistency that manual processes cannot match. Beyond this, fully advanced automated welding is being progressively phased into our production lines – a meaningful upgrade in output speed and weld quality repeatability. On the design side, Tekla Structures enables direct CNC cutting file output without re-entry, removing a key source of error and delay. Together, these investments allow throughput to scale without a proportional increase in headcount – critical when skilled fabrication supervisors are in short supply industry-wide.
How does Salasar balance thermal orders with renewable infrastructure work, given grid stability priorities?
Thermal and renewable are complementary in our order book, not competing. Thermal power continues to account for approximately 50 per cent of India’s installed capacity and remains essential for baseload stability, while renewable capacity grows in parallel – and both are structural steel-intensive. Our portfolio spans transmission towers, substation structures, solar mounting structures, railway electrification, and heavy plant structures, which means our manufacturing lines remain loaded continuously even when one segment slows. Thermal orders tend to be larger, longer-lead, and higher-value per project; renewable orders are higher-volume with faster cycle times. We manage these as distinct but parallel pipelines with dedicated capacity allocation, rather than competing for the same resources.
What KPIs – such as fabrication yield, on-time delivery rates, or defect ppm – demonstrate your edge in thermal structures?
The KPIs that matter most to our clients are dimensional accuracy, weld quality first-pass acceptance rates, and on-site fit-up performance. We track weld defect rates through radiographic and ultrasonic testing, with zero defects. Fabrication yield – the ratio of input steel to shipped steel accounting for offcuts and scrap – is a meaningful cost indicator; at our scale, even a one percentage point improvement translates to significant annual savings. On dispatch, our benchmark is adherence to committed monthly tonnage within ±5 per cent, which aligns with the tolerance most EPC contractors build into their erection schedules. Fit-up quality at the site – structures requiring excessive shimming or rework – is equally tracked, and our CNC investment directly addresses this.
How do you ensure quality certification alignment with international standards like ASME for exported components?
Salasar is currently executing transmission projects in Rwanda and Nepal, with an overseas strategy focused on markets offering visible infrastructure demand and room for Indian EPC players with integrated capabilities. In heavy structures, our international footprint spans multiple geographies, from the Greater Malé Connectivity project in the Maldives through Afcons Infrastructure to PEB warehouse structures in Fiji and machinery support structures in Germany – each market carrying its own certification and quality expectations, which our systems are built to accommodate.
We adhere to AWS D1.1 for structural weld quality – the standard most commonly demanded in international markets, including the Gulf – and to ASME Section IX for welding procedure and welder qualification on process plant-adjacent work. We qualify our welding procedures and welders against multiple codes simultaneously, enabling our teams to execute to IS, ASME, or AWS standards without fresh qualification delays for each order. Third-party inspection is standard on all export orders, facilitated within our production schedule rather than as a separate disruption.
Which segments of thermal expansion – brownfield retrofits or greenfield plants – offer the highest margins, and why?
Brownfield retrofits command higher margins because of complexity. Our gallery re-routing and dismantling work for Blast Furnace-3 at JSW’s Dolvi plant in Maharashtra – 2,000 MT executed within a live, operating facility – illustrates this precisely. Every lift and new structural member had to be planned around running equipment with no room for schedule slippage. Engineering effort per tonne is substantially higher, and the execution risk premium is justified.
Greenfield projects at the scale of today’s 800 MW USC units are compelling in volume – a single unit can represent thousands of tonnes of structural steel – with more predictable planning horizons. Our strategy is to pursue both: greenfield for volume and Tier-1 EPC relationships and brownfield for value capture and direct client engagement.
What role do EPC contractors play in standardising specifications across developers?
EPC contractors are the de facto standardising force in India’s thermal power sector. When a developer like NTPC or Adani Power engages a primary EPC – L&T, BHEL, or an international specialist – that EPC’s technical requirements cascade through the entire supply chain, covering dimensional tolerances, weld quality, surface preparation, and marking standards consistently across projects. For a manufacturer like Salasar, this is beneficial – it reduces the proliferation of bespoke requirements. Over time, we have internalised these requirements into our shop procedures, making compliance a matter of process rather than a fresh exercise per order. The broader trend toward standardised 660 MW and 800 MW unit sizes reinforces this further, enabling design rationalisation that should eventually translate into specification alignment across EPCs as well.
By 2030, how will policy shifts towards cleaner coal technologies reshape demand for your structures?
The government’s recent revision exempting 78 per cent of thermal power plants from mandatory FGD installation reflects the balancing act between environmental targets and the pace of thermal expansion. The structural direction, however, is clear: all new capacity being tendered is USC or, going forward, AUSC (advanced ultra-supercritical), requiring progressively more sophisticated structural steel solutions. Cleaner coal also means flue gas treatment where mandated, ash handling upgrades, and cooling tower modifications – all structural steel-intensive. The growing shift toward flexible thermal operation, where plants ramp to balance renewable intermittency, introduces fatigue loading as a new structural design consideration – one we are actively factoring into our engineering inputs. By 2030, demand for structural steel in thermal will be defined by quality and specialisation rather than volume alone.
What separates engineering firms that thrive in baseload revival from those that do not?
Three factors consistently differentiate firms that capitalise on a demand cycle. First, integrated capability – engineering, manufacturing, and dispatch under one roof, without multi-vendor handoffs. Our track record reflects this at scale: the 7,353 MT Adani boiler structure at Anuppur, 5,554 MT BOP structures for AMNS in Gujarat, and 5,500 MT steel plant structures for JSW-BPSL at Sambalpur and Jharsuguda are all executed projects with clients who do not tolerate gaps.
Second, financial depth. Large thermal orders carry significant working capital demands before the first invoice clears. Firms without the balance sheet to absorb procurement and production costs ahead of billing cannot scale even when orders are available.
Third and most underappreciated is people and systems. Thermal structural manufacturing is a specialist discipline. Supervisors who understand the interface between structural steel and process plant equipment are not produced quickly. Investing in this talent through lean cycles is what allows rapid mobilisation when the market accelerates. The firms that endure are those that treat capability building as a constant, not a reaction to demand.
Posted On